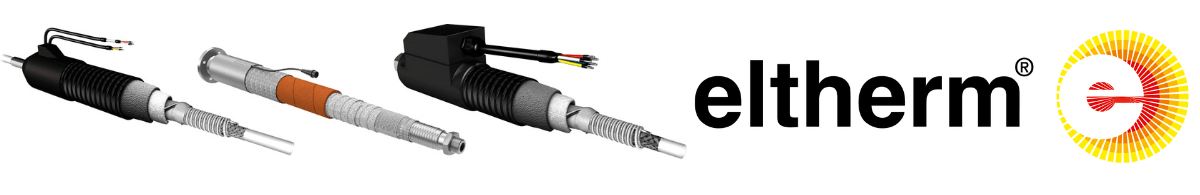
Introduction: Why Heated Hoses Are Critical in Industrial Applications
A heated hose plays an essential role in maintaining the temperature of fluids and gaseous media during the transfer in industries such as food processing, pharmaceuticals, chemicals, and automotive manufacturing. Whether it’s transporting viscous adhesives or temperature-sensitive liquids, precision heat control is vital to maintaining product integrity and operational efficiency.
However, industries that use heated hoses face their own unique challenges—ranging from environmental durability to regulatory compliance. Fortunately, companies like Eltherm have developed advanced solutions to overcome these hurdles.
In this article, we explore the six most common challenges in heated hose applications in process industries and how Thorne & Derrick together with Eltherm’s technology leads the way in solving them.
Durability and Reliability in Harsh Environments
Many heated hoses must operate in environments with high mechanical stress, extreme temperatures, or chemical exposure. Durability is crucial for long-term performance.
Solution:
-
Uses high-grade materials such as PTFE, silicone, and stainless steel braiding
-
Designs hoses to withstand abrasion, UV exposure, and chemical corrosion
-
Conducts rigorous testing to ensure performance across harsh industrial settings
️Precise and Stable Temperature Control
Accurate temperature maintenance is critical in industries where a few degrees can affect fluid viscosity or product quality.
Solution:
-
Integrates advanced temperature sensors like RTDs and thermocouples
-
Offers digital control units for precise temperature monitoring
-
Customises heated hose designs for both constant wattage and self-regulating heating technologies
Customisation for Diverse Industrial Needs
Off-the-shelf heated hoses often don’t meet the specific requirements of various industries, especially in terms of length, connectors, and heating parameters.
Solution:
-
Provides fully customised heated hose systems tailored to client specifications
-
Supports various end fittings, insulation types, and temperature ranges
-
Modular design allows easy integration into existing production lines
️Compliance with Industry Standards
Safety and quality regulations vary by industry and geography. From ATEX zones to FDA approval, compliance is non-negotiable.
Solution:
-
Designs heated hoses to meet international standards like ATEX, IECEx, and FDA
-
Offers full certification support for regulatory approval
-
Supplies explosion-proof and food-grade heated hose variants
Energy Efficiency and Sustainability
Heating systems can consume significant energy, impacting operational costs and sustainability goals.
Solution:
-
Uses self-regulating heating cables to reduce power consumption
-
Provides high-efficiency insulation to minimise heat loss
-
Continuously improves energy performance to lower the carbon footprint of heated hose systems
️Reducing Maintenance and Downtime
Unplanned downtime due to hose failure can disrupt production and cause financial losses.
Solution:
-
Builds heated hoses for longevity and low maintenance
-
Incorporates diagnostic and predictive maintenance technologies
-
Designs quick-connect systems for faster servicing and minimal disruption
Conclusion: A Smarter Way to Heat with eltherm
As demand grows for smart, efficient, and reliable heated hose solutions, Eltherm remains at the forefront of innovation. Their deep expertise in thermal management, engineering flexibility, and commitment to compliance make them a trusted partner across industries.
Whether you’re in food manufacturing, chemical processing, or automotive production, Eltherm’s heated hose systems supplied by Thorne & Derrick deliver unmatched precision, durability, and value.
Looking for a custom heated hose solution? – Contact Thorne & Derrick’s experts today.

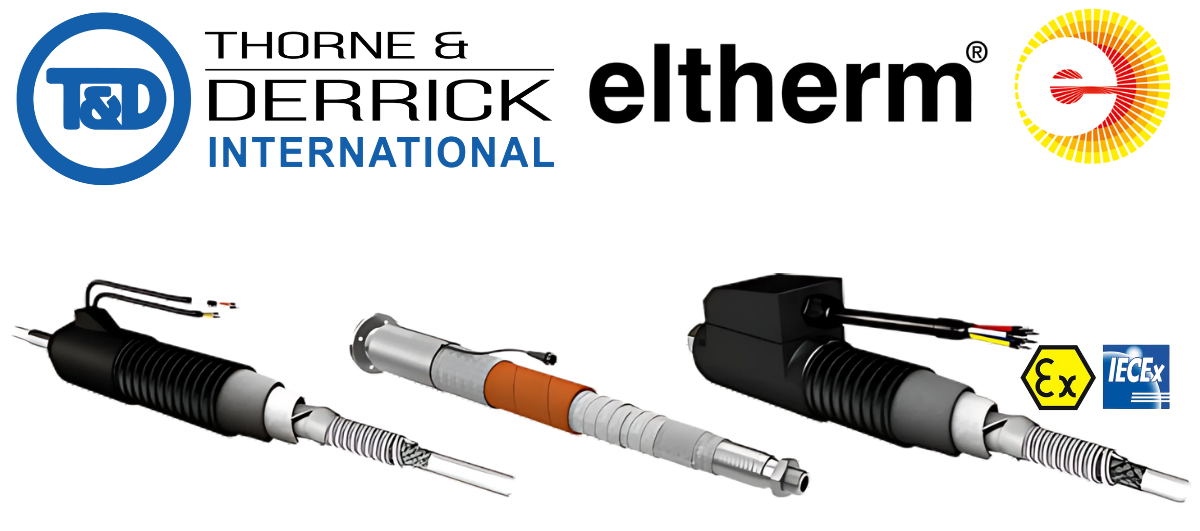
Bespoke Hose Designs | 40+ Years Experience from Process Heating Specialists
Heated Hose
When it comes to maintaining the safe and efficient transfer of liquids or gases in extreme conditions, a heated hose is an indispensable tool. Designed to ensure media temperature stability, heated hoses are essential in industries where process reliability and product integrity are paramount.
Whether you’re transporting adhesives, water, chemicals, food-grade materials, or gas, a heated hose prevents blockages, freezing, and viscosity changes — all of which can seriously disrupt operations.
So what exactly is a Heated Hose?
A heated hose is a flexible, insulated hose that incorporates an integrated heating element. This heating cable runs along the hose, controlled by thermostats or external temperature controllers to maintain the desired setpoint.
Heated Hose Components:
-
Inner Hose: Typically made of PTFE, silicone, or stainless steel for chemical resistance
-
Heating Element: Eltherm’s cutting-edge technology ensures even heat distribution
-
Insulation Layer: Prevents heat loss and ensures efficiency
-
Outer Jacket: Durable and resistant to weather, chemicals, and mechanical stress
Common Industrial Applications for a Heated Hose
Industrial operations often rely on precise temperature control to ensure product integrity, efficiency, and safety. Heated hoses are used across various sectors:
- Food & Bev: Maintain hygienic temperature control for chocolate, syrup, and dairy products
- Chemical Processing: Safe handling of temperature-sensitive chemicals and solvents
- Pharmaceuticals: Ensure stable temperatures for bio-materials and liquid medicines
- Gas Transfer: Prevent condensation or freezing of gases like nitrogen or CO₂
- 3D Printing & Plastics: Maintain polymer flow for consistent extrusion
Choosing the Right Hose
Manufactured by Eltherm, a global leader in electrical heat tracing, our heated hoses are engineered to the highest German quality standards. Known for reliability and innovation, Eltherm hoses deliver:
-
Temperature range: Ensure the hose supports the necessary operating temperature
-
Chemical compatibility: The inner tubing material must resist corrosion or degradation from the media
-
Length and flexibility: Choose a length and bend radius suitable for your setup
-
Certifications: Look for compliance with industry standards (ATEX-certified options for explosive atmospheres)
Buy Heated Hoses from Thorne & Derrick
Heated hoses are more than just a winter solution—they’re a vital piece of equipment for maintaining operational efficiency and product quality in a wide range of industrial applications. Investing in the right heated hose can lead to fewer stoppages, less waste, and greater control over your process.
As an official distributor of Eltherm products, Thorne & Derrick provides expert support and a comprehensive range of heated hoses for both liquid and gas applications. We work closely with clients to specify the exact hose configuration for your needs, including temperature requirements, pressure ratings, and fitting.
Not sure which heated hose is right for your application? Get in touch with our specialists — we’ll guide you from specification to installation.
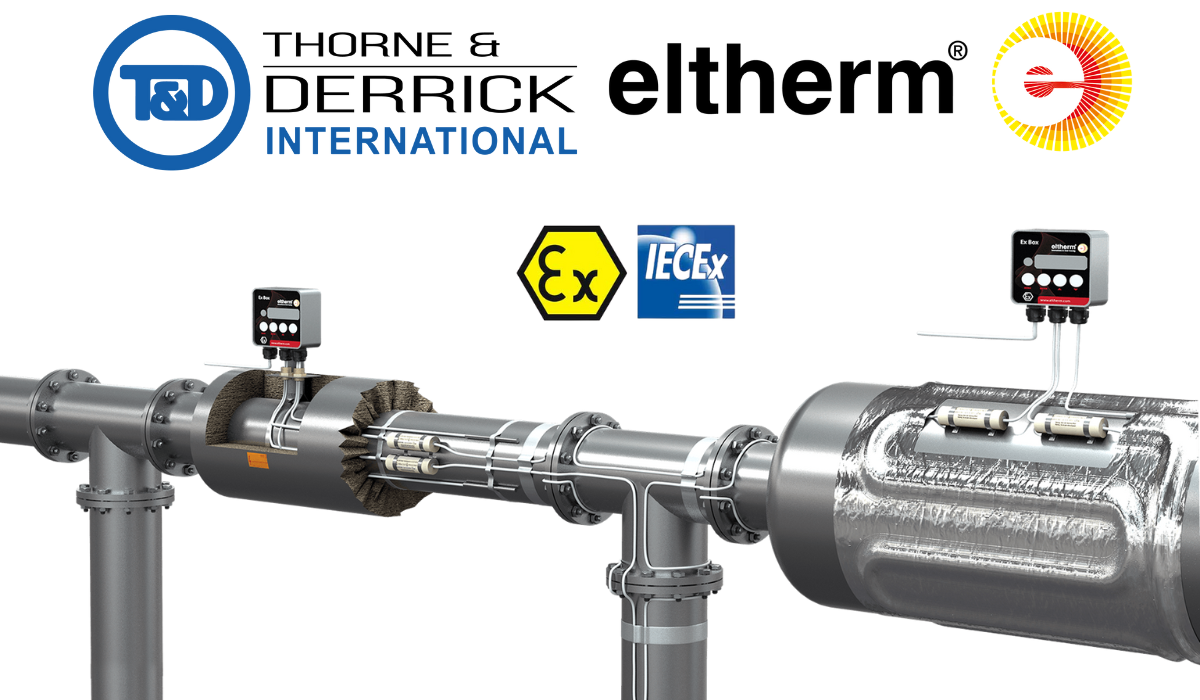
Heat Tracing Solutions
Competitive Pricing | UK Heat Trace Stockist & Supplier | Industrial & Hazardous Areas
At Thorne & Derrick, we understand that heat tracing plays a critical role in many industries, ensuring the safety and efficiency of processes by preventing freezing, regulating temperatures, and safeguarding equipment. However, like any industrial system, trace heating can present its challenges, ranging from improper installation and poor maintenance to energy inefficiencies and safety risks. Fortunately, with our comprehensive range of products and expert services, we’re well-equipped to address these challenges head-on.
In this blog, we’ll walk you through some of the most common challenges in heat tracing applications—and how our solutions help clients overcome them to ensure maximum performance and reliability.
1. Improper Installation
Improper installation of heat tracing systems is one of the most frequent challenges. Incorrect cable placement, poor terminations, or choosing the wrong type of system can lead to uneven heat distribution, overheating, or system failure.
How We Help:
-
Product Selection Support: We provide expert advice to ensure that the right products—whether cables, controllers, or accessories—are selected based on your specific needs. Our team works closely with you to make sure the system is tailored to your application.
-
Training & Installation Guidance: Our experts offer on-site support and training to your installation teams, ensuring cables are spaced correctly, terminations are properly done, and all connections are safe and secure.
2. Poor Maintenance and Inspection
Regular maintenance and inspection are key to keeping trace heating systems running smoothly. Over time, heat trace cables can become damaged, and components may degrade, which can impact the overall performance of the system.
How We Help:
-
Spare Parts & Components: We provide a wide variety of high-quality replacement parts such as cables, thermostats, and sensors, so you can quickly address any issues and ensure the reliability of your systems.
-
Preventive Maintenance Kits: We offer tools and diagnostic equipment to help you carry out regular inspections and proactive maintenance, minimizing the risk of system failure before it impacts operations.
3. Overheating and Underheating
If your trace heating system is either overheating or underheating, it can lead to equipment damage or operational inefficiencies. Overheating can cause insulation degradation, while underheating may fail to protect pipes from freezing in colder conditions.
How We Help:
-
Advanced Temperature Controllers: Our precise control systems allow for accurate regulation of your trace heating system, ensuring temperatures remain within the desired range and preventing overheating or underheating.
-
Self-Regulating Cables: We offer self-regulating cables that adjust their heat output based on the temperature of the surface they are attached to, ensuring consistent and energy-efficient heating.
4. Control System Failures
Heat Trace Systems rely on sensors and thermostats to regulate temperature. When these components malfunction, your entire system can be thrown off balance.
How We Help:
-
Integrated Control Solutions: We offer advanced control panels and monitoring systems to keep your trace heating system running smoothly. These solutions prevent failures by providing real-time monitoring, enabling immediate action if something goes wrong.
-
Remote Monitoring & Alerts: For added convenience, our remote monitoring solutions allow you to track the performance of your trace heating system from anywhere, ensuring that potential issues are caught before they lead to system downtime.
5. Energy Efficiency and Cost
These systems are often energy-intensive. Without optimisation, they can drive up operational costs, leading to higher electricity bills.
How We Help:
-
Energy-Efficient Products: We provide energy-efficient solutions, such as self-regulating cables and smart controllers, to help reduce energy consumption and lower your operational costs.
-
Cost-Effective Solutions: With a wide range of trace heating products available, we ensure that you can find the most cost-effective solution that meets your performance needs and fits within your budget.
6. Corrosion and Environmental Factors
Trace heating systems in harsh environments—such as offshore platforms or chemical processing plants—can be exposed to corrosive elements, aggressive weather, or chemicals. These factors can degrade the cables and components over time.
How We Help:
-
Corrosion-Resistant Products: We supply trace heating cables and components made from durable materials designed to resist corrosion, ensuring your systems last longer in harsh conditions.
-
Hazardous Area Equipment: For applications in explosive or hazardous environments, we offer certified trace heating solutions that meet ATEX and IECEx standards, ensuring both safety and durability.
7. Regulatory and Safety Compliance
They must comply with various safety regulations and standards. Non-compliance can lead to safety hazards or costly legal issues.
How We Help:
-
Safety-Certified Products: All of our trace heating products meet the latest industry standards and regulations, including ATEX and IECEx certifications, ensuring that your systems are both safe and compliant.
-
Documentation & Certification: We provide full product certification and installation documentation to help you meet regulatory requirements with ease.
8. Freezing and Blockages
In cold environments, systems are often used to prevent freezing in pipes and vessels. If these systems fail to maintain the required temperature, it can lead to costly damage, downtime, and even safety risks.
How We Help:
-
Freeze Protection Systems: We offer specialised solutions designed to prevent freezing in pipes, keeping your systems operational even in extreme temperatures.
-
Flow Assurance: Our heating solutions help prevent blockages caused by solidified fluids, ensuring smooth operation and minimising downtime.
9. Complexity in Retrofitting Existing Systems
When retrofitting older systems, compatibility issues can arise, especially when trying to integrate new components with legacy infrastructure.
How We Help:
-
Retrofit Solutions: We offer flexible trace heating products that are easy to integrate into existing systems. Whether upgrading or expanding, our solutions are designed to work with your legacy equipment.
-
Custom Solutions: Our team can customise to meet the unique requirements of your existing infrastructure, making the retrofit process easier and more efficient.
10. System Integration and Compatibility Issues
Integrating trace heating with other industrial systems, like HVAC or process heating, can sometimes lead to compatibility problems, affecting the overall performance of your operation.
How We Help:
-
Custom Integration Solutions: We specialise in providing systems that integrate seamlessly with other systems, ensuring smooth operation and minimising disruptions.
-
Expert Guidance: With our extensive industry experience, we offer expert advice to ensure that your trace heating system is compatible with existing processes and automation systems.
11. Environmental Impact
As businesses continue to focus on sustainability, reducing the environmental impact of industrial operations is more important than ever.
How We Help:
-
Sustainable Solutions: Our energy-efficient trace heating products are designed to help reduce energy consumption, making your operations more sustainable and cost-effective.
-
Recyclable Materials: We offer trace heating components made from recyclable materials, helping your business reduce its carbon footprint.
12. Cost of Materials and Components
The cost can be a concern, especially for large-scale installations or retrofitting projects.
How We Help:
-
Competitive Pricing: We offer products at competitive prices, ensuring that you can find the right solution within your budget.
-
Long-Term Value: Our high-quality, durable products are designed to minimise the need for frequent replacements, providing excellent long-term value.
Conclusion
At Thorne & Derrick, we understand the complexities and demands of certain heat tracing applications and are dedicated to helping our clients overcome challenges with confidence. Trace heating systems are essential to the safety, efficiency, and reliability of operations across numerous industries—but only when installed, maintained, and managed correctly.
Whether you’re planning a new installation, upgrading legacy infrastructure, or looking to optimise performance, our team is ready to help you unlock the full potential of your trace heating system.
Get in touch with us today to discover how we can help you achieve safer, more efficient, and compliant operations.
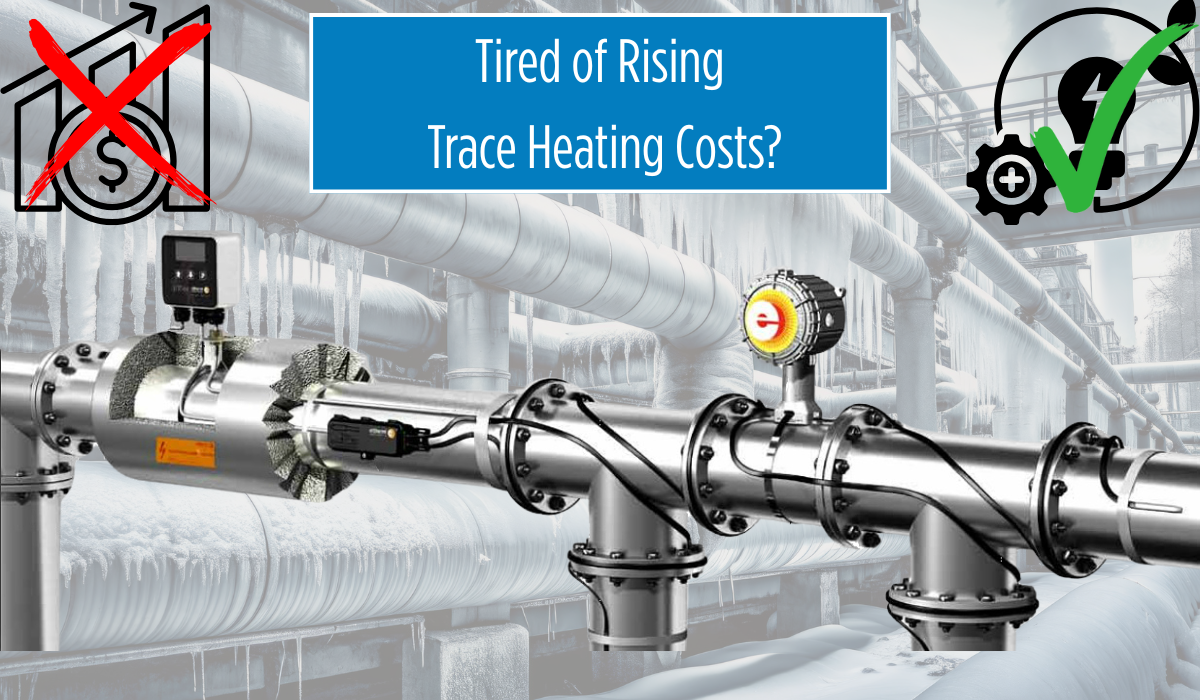
Rising Trace Heating Costs
In recent years, the cost of trace heating systems has continued to rise — particularly with well-known market leaders. For engineers, specifiers, and procurement professionals under increasing budget constraints, this presents a challenge: how to maintain system performance, safety, and compliance without escalating costs.
Whether you’re planning a new installation or reviewing procurement options, we can support you with detailed technical specs, design assistance, and competitive pricing that makes sense for your project and your budget.
At Thorne & Derrick, we believe that you shouldn’t have to compromise on quality to control your budget. We work closely with our clients across industries who are looking for a better balance of value and performance. That’s why we’re highlighting Eltherm, German-engineered trace heating solutions that offer technical equivalence to market leaders, with the added benefit of greater cost-efficiency.
Why Consider eltherm?
Eltherm is a globally trusted manufacturer offering high-performance heat trace systems designed for frost protection, process temperature maintenance, and critical process applications across a range of industries. Built for reliability in demanding conditions, Eltherm systems meet and often exceed international standards.
Key benefits include:
-
Technical performance equal to market leaders
-
Full compliance with ATEX, IECEx, and international safety standards
-
Custom-engineered solutions for complex or hazardous applications
-
Significant cost savings without compromise on quality or lifespan
Whether you’re planning a new build, retrofitting an existing facility, or simply exploring options beyond the usual names, Eltherm is a smart choice backed by proven results in oil & gas, chemical processing, utilities, and industrial manufacturing.
Why Choose Thorne & Derrick for Your Trace Heating Solutions?
With over four decades of experience, Thorne & Derrick has supplied and supported trace heating systems across the UK and international markets. Our in-house technical experts provide tailored design support, installation guidance, and product specification across a wide range of sectors — including energy, utilities, manufacturing, and process industries.
We don’t just supply equipment — we support your project from concept to commissioning, ensuring system integrity and long-term operational success.
-
Custom Solutions: Tailored trace heating designs for temperature maintenance and frost protection
-
Innovative Products: Latest-generation self-regulating cables certified for explosive environments
-
Fast Delivery: Largest UK stock with next-day delivery
-
Expert Support: Free heat loss calculations and design services to optimise your system.
-
Certified Engineers: CompEx-trained staff ensure safe and reliable system design and implementation
Get in Touch Today
If you’re reviewing your current trace heating solutions or planning future projects, now is the time to consider alternatives. Tired of rising trace heating costs?
Contact us today to discuss your application and see how Eltherm can deliver uncompromising performance at a more competitive price point.
What is Trace Heating?
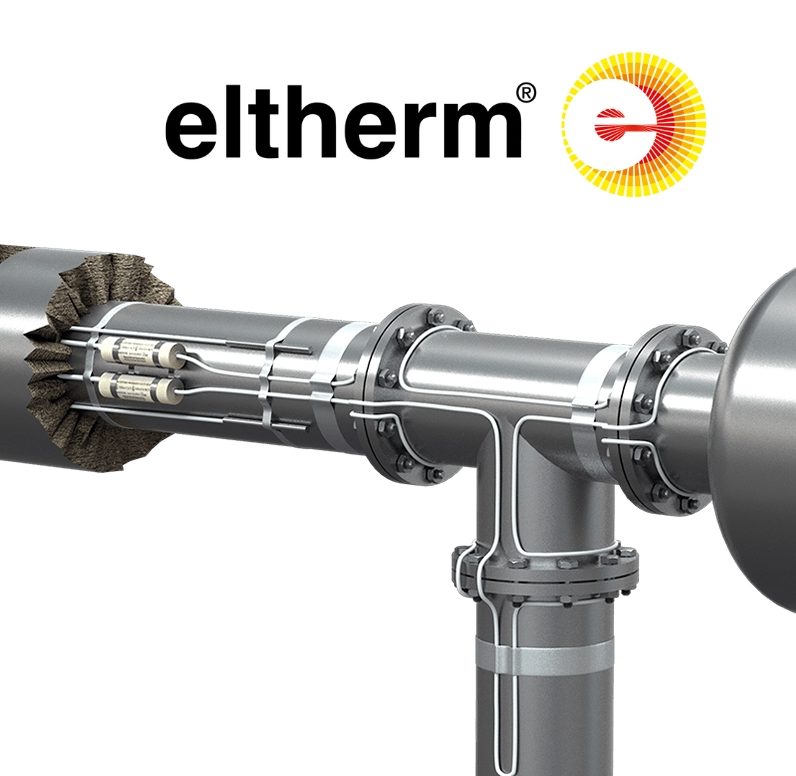
Trace heating, is an electrical system used to maintain or raise the temperature of pipes, vessels, and equipment by compensating for heat losses. Trace Heating involves running specially designed heating cables along the length of the pipe or around equipment, providing direct, controlled heat to ensure fluid movement and process stability in industrial environments.
So, what is trace heating? Trace heating is the application of electrical heat to pipes or surfaces, typically for freeze protection or temperature maintenance. Whether you’re searching for “what is a heating cable” or “what is trace heating,” you’re referring to the same vital temperature control solution used in sectors like oil & gas, chemical processing, power generation, and food production.
At its core, trace heating is about maintaining process integrity—ensuring that fluids don’t freeze, solidify, or drop below the required temperature, even in harsh or hazardous environments.
Need to know more about Heat Trace Systems and whether it’s essential for your business?
How Does Trace Heating Work?
Trace heating systems work by converting electrical energy into heat through resistance. The heating cable is secured directly to the pipe or tank surface, and when powered, it generates heat that offsets thermal loss. Most industrial systems include:
-
Heating cable (self-regulating, constant wattage, etc.)
-
Thermal insulation over the assembly
-
Temperature sensors and control units
-
Power distribution and monitoring systems
A key advantage in industrial environments is the level of control: temperatures can be precisely managed through thermostats or sophisticated process controllers to align with specific process requirements.
Types of Trace Heating Cables
Different trace heating technologies are designed for varying industrial and commercial needs—ranging from freeze protection to high-temperature process maintenance.
1. Self-Regulating Trace Heating Cables
-
Function: Adjust heat output based on ambient or pipe temperature.
-
Use Cases: Ideal for freeze protection, tank farms, and pipelines with variable ambient conditions.
-
Advantages: Energy-efficient, safe from overheating, and suitable for hazardous areas.
2. Constant Wattage Trace Heating Cables
-
Function: Deliver uniform heat output along their length.
-
Use Cases: Good for longer pipe runs with consistent heat demand—e.g. long distillation lines or storage tank manifolds.
-
Advantages: Cost-effective, scalable for large plants.
3. Series Resistance Trace Heating Cables
-
Function: Use a resistive heating wire that emits heat when powered.
-
Use Cases: Large-scale industrial environments requiring high wattage and long continuous runs, such as petrochemical pipelines.
-
Advantages: High performance, ideal for long-distance runs with few power supply points.
4. Mineral Insulated (MI) Trace Heating Cables
-
Function: Extremely durable heating cable with a metal sheath and magnesium oxide insulation.
-
Use Cases: Heavy industrial sectors—nuclear, oil & gas, or environments with exposure to high temperatures and corrosive elements.
-
Advantages: High temperature tolerance (up to 600°C), long lifespan, and superior mechanical protection.


How Can Trace Heating Be Applied?
While trace heating can be found in some commercial environments (e.g. hotel water systems or gutter de-icing), its primary value lies in industrial applications. Key sectors include:
Oil & Gas
-
Prevent wax, hydrate, or water blockages in pipelines
-
Maintain flow assurance in offshore and onshore operations
-
Trace heating of valves, pumps, and metering equipment in hazardous zones
Chemical & Petrochemical Plants
-
Maintain critical process temperatures for viscous or temperature-sensitive fluids
-
Ensure safety and product integrity in reactor and separator systems
-
Temperature control for corrosive or hazardous material pipelines
Food & Beverage Processing
-
Keep edible oils, chocolate, syrups, and other viscous materials at flowable temperatures
-
Prevent crystallisation or solidification during transfer and storage
-
Maintain temperature-sensitive CIP (Clean-in-Place) systems
Power Generation
-
Protect demineralised water lines in boiler feed systems
-
Maintain lubricant viscosity in turbines and rotating equipment
-
Prevent freezing in fire protection and cooling water lines
Pharmaceuticals & Biotech
-
Precise temperature control of fluids during batch production
-
Sanitary process line heating without risk of contamination
-
Support for temperature-sensitive reactions and formulations
Mining & Minerals
-
Prevent freezing or viscosity drops in process slurry pipelines
-
Trace heating of reagent lines or tank heating in leaching operations
-
Maintain flow in exposed areas subject to extreme climates
Why Is Trace Heating Needed?
In industrial and commercial environments, failure to maintain temperature can lead to:
-
Equipment damage due to freezing or overheating
-
Blockages and flow interruptions
-
Increased maintenance costs
-
Health and safety risks (especially in flammable or toxic applications)
-
Lost production time
Industrial trace heating ensures operational continuity, product quality, and safety—especially in hazardous or extreme environments.
Key Benefits of Trace Heating Systems
✅ Operational Reliability – Prevent flow issues and freezing, especially in mission-critical infrastructure
✅ Process Integrity – Maintain consistent product quality through controlled thermal environments
✅ Energy Efficiency – Especially with self-regulating or sensor-driven systems
✅ Customisability – Scalable for large industrial plants and suitable for hazardous area classifications (ATEX, IECEx)
✅ Longevity – High-durability options like MI cables can last decades with minimal maintenance
Need A Trace Heating Solution?
With over 40 years of experience in the industry, Thorne & Derrick are trusted specialists in trace heating solutions across all industrial sectors. Our team delivers tailored systems that meet the unique demands of your application—whether for hazardous areas, extreme environments, or precision process control.
We offer in-house heat loss calculations, full system design, and technical specification, using only high-performance, market-leading heating cables and components. From concept to commissioning, our focus is on delivering cost-effective, engineered solutions that reduce downtime, optimise performance, and drive long-term project success.
Thorne & Derrick are the UK’s largest stockist and supplier of Trace Heating products, including ATEX Heat Tracing Cables, Heated Hoses, Heating Mats & Jackets, Drum Heaters, IBC Heaters & more.