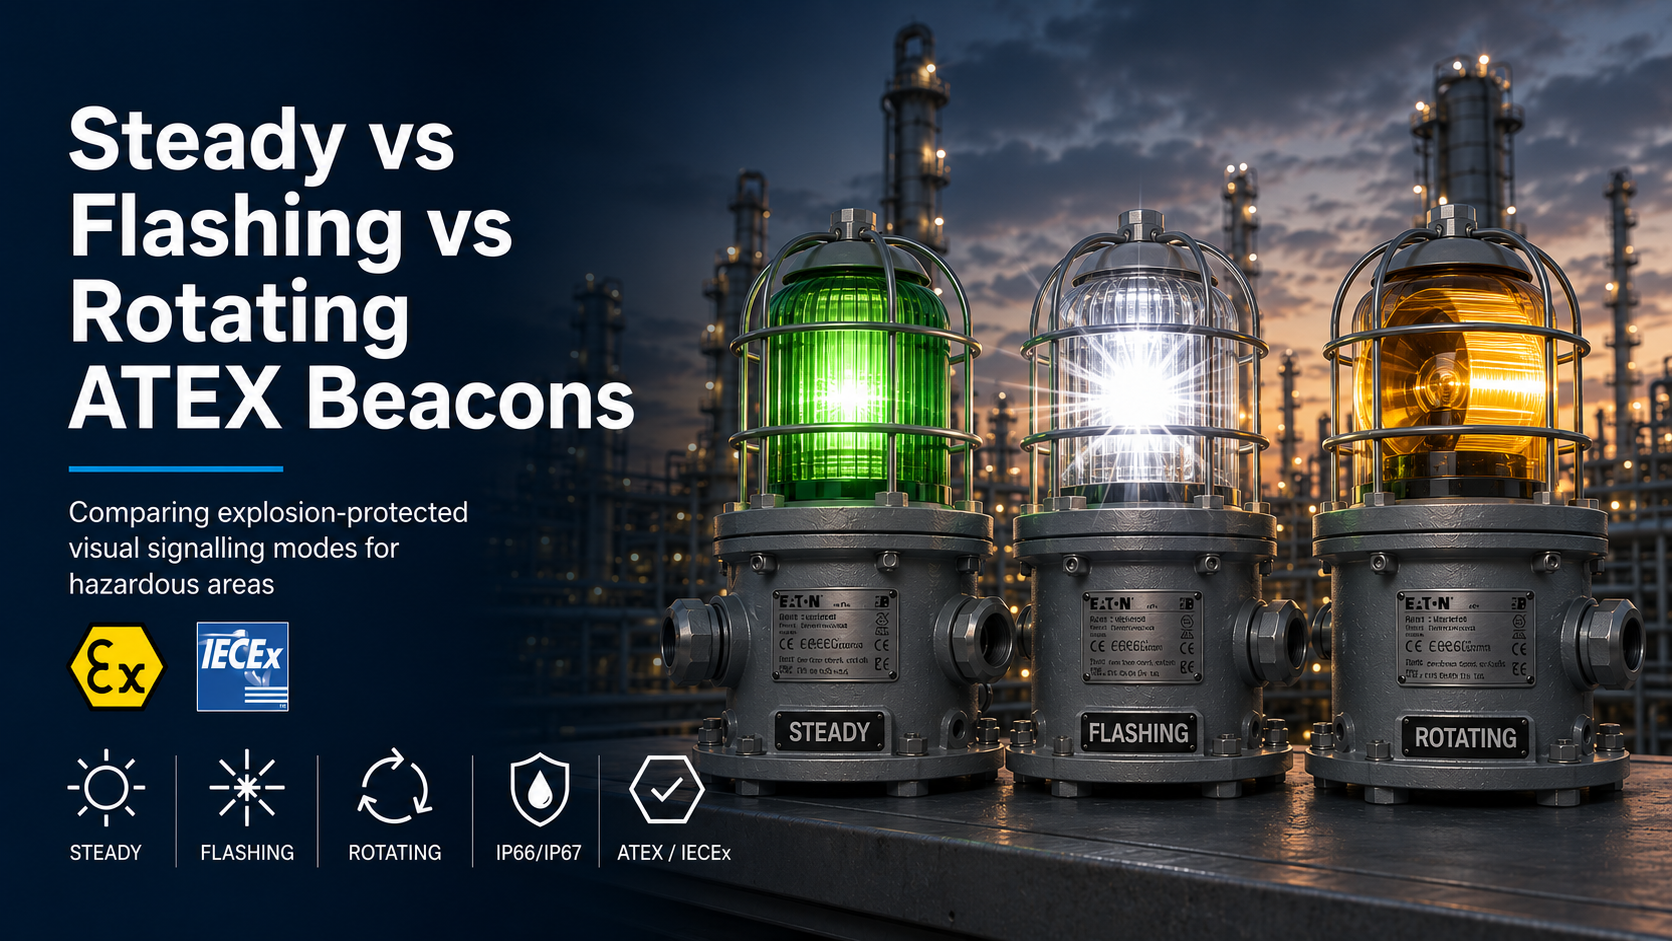
Steady, flashing, strobe and rotating beacons communicate different types of warning and status information. Although each produces a visible signal, the way that signal attracts attention and conveys meaning can vary considerably.
A steady beacon provides continuous illumination. A flashing beacon switches between illuminated and non-illuminated states. A strobe beacon produces brief, high-intensity pulses, while a rotating beacon creates the appearance of a moving light.
Thorne & Derrick supplies a comprehensive range of hazardous area ATEX beacons with steady, blinking, strobe, xenon-flash and electronically rotating visual signals.
For an introduction to hazardous area visual signalling, read What Is an ATEX Beacon?
Quick answer: use steady illumination for persistent status indication, flashing or strobe signals where increased attention is required, and rotating signals where a distinctive moving visual warning supports the site alarm philosophy.
Steady vs Flashing vs Rotating Beacons: Quick Comparison
| Signal Mode |
Visual Behaviour |
Typical Purpose |
Important Selection Data |
| Steady |
Continuous illumination |
Persistent equipment, plant or process status |
Optical output, colour, viewing distance and continuous-duty rating |
| Flashing or Blinking |
Repeating on-and-off pattern |
Warning, changing condition or attention signal |
Flash frequency, duty cycle, colour and control method |
| Strobe |
Brief, rapid or high-intensity pulses |
Prominent alarm or emergency warning |
Flash energy or optical intensity, frequency and current consumption |
| Rotating |
Moving beam or electronically sequenced segments |
Distinctive warning or recognisable plant-status signal |
Rotation rate, field of view, mechanism and maintenance requirements |
Important: the most attention-grabbing signal is not automatically the correct choice. The selected mode must agree with the site alarm philosophy and remain distinguishable from other alarms and equipment-status indicators.
When Should a Steady Beacon Be Used?
A steady beacon remains illuminated while the electrical supply or control signal is present. It provides a continuous reference rather than repeatedly attracting attention through movement or flashing.
This makes steady signalling particularly useful for showing a persistent operating state or condition.
Typical Steady-Beacon Applications
- Equipment running or stopped indication
- Valve open or closed status
- Process available, isolated or inhibited condition
- Persistent local warning
- Plant or machinery status indication
- A visual signal designed to remain active for an extended period
Advantages of Steady Illumination
- Provides a constant visual reference
- Suitable for persistent process and equipment states
- Can be easier to interpret where several flashing alarms are present
- Available using filament, fluorescent or LED technologies, depending on the product
Limitations of a Steady Signal
Continuous illumination may attract less immediate attention than a changing or moving signal. A steady beacon can also become part of the visual background where several continuously illuminated indicators are present.
Viewing distance, mounting position, lens colour and contrast against the surrounding environment should therefore be assessed.
When Should a Flashing or Blinking Beacon Be Used?
A flashing or blinking beacon changes between illuminated and non-illuminated states at a defined frequency. The changing light level can attract more attention than a steady signal.
In many LED products, the pattern is produced electronically. The flash rate may be fixed or selected from the modes available within the product.
Typical Flashing-Beacon Applications
- Process alarm or fault condition
- Equipment trip or abnormal status
- Gas, fire or evacuation warning
- Attention signal before machinery starts
- Condition requiring operator acknowledgement
Flash Frequency
Flash frequency describes how often the signal repeats. The correct frequency should be determined by the product capability and site alarm philosophy.
Two alarms with similar colours and flash frequencies may be difficult to distinguish. Signal patterns should therefore be coordinated across the installation.
What Is the Difference Between Flashing and Strobe?
“Flashing” is a broad description for a light that repeatedly switches on and off. A strobe is a more specific type of flashing signal that produces brief and often high-intensity pulses.
A xenon strobe discharges stored electrical energy through a xenon flash tube. Its output is commonly specified using flash energy in joules and flash frequency.
An LED strobe creates its pulse electronically. Its optical performance is not automatically equivalent to a xenon flash with a stated joule rating.
| Comparison |
LED Strobe |
Xenon Strobe |
| Light source |
Light-emitting diodes |
Xenon flash tube |
| Signal generation |
Electronically controlled LED pulses |
Discharge of stored electrical energy |
| Common performance data |
Optical intensity, pattern and pulse frequency |
Flash energy in joules and flash frequency |
For a fuller technology comparison, read LED vs Xenon ATEX Beacons.
How Does a Rotating Beacon Work?
A rotating beacon creates a moving visual signal that appears to sweep around the installation. This movement can make the signal recognisable even where several fixed lights are present.
Rotating signals can be produced mechanically or electronically.
Mechanically Rotating Beacons
A mechanically rotating design uses a motor and rotating reflector or light assembly to direct the beam around the beacon.
Rotation speed, motor life and moving-part maintenance should be considered when specifying this type of product.
Electronically Rotating LED Beacons
An electronically rotating beacon illuminates LED segments in sequence. This creates the appearance of movement without a motor-driven reflector.
Different electronic rotation patterns or speeds may be available, depending on the model.
Typical Rotating-Beacon Applications
- Distinctive plant or machinery warning
- Vehicle, loading or movement indication
- Process condition requiring a recognisable moving signal
- Replacement of an established rotating-beacon alarm convention
Which Signal Is Most Visible?
No single signal mode is the most visible under every condition. Visibility depends on the product output, signal pattern and installation environment.
Consider:
- Viewing distance
- Ambient lighting and direct sunlight
- Mounting height and orientation
- Structures and process equipment that may obstruct the signal
- Required horizontal and vertical field of view
- Lens or LED colour
- Flash or rotation frequency
- Other visual signals in the same area
The product should be positioned so that the intended audience can see and interpret the signal from the required working locations.
Does Each Signal Mode Have a Fixed Meaning?
A signal mode does not automatically carry one universal meaning across every site. Its purpose should be defined within the alarm philosophy, operating procedure or project specification.
For example, one installation may use steady illumination for normal equipment status and flashing red for an alarm. Another site may reserve flashing signals for evacuation and use rotating amber for machinery movement.
The meaning must therefore be documented, communicated to personnel and applied consistently.
How Does Lens Colour Affect the Signal?
Lens or LED colour helps distinguish between alarm and status conditions, but it can also affect the apparent optical output.
The visibility of red, amber, green, blue, yellow or clear signals can differ according to the light source, lens construction and surrounding lighting.
Manufacturer performance data should be checked for the exact ordered colour.
Electrical Supply and Control Considerations
Signal mode can affect the beacon’s current consumption and control requirements. The exact electrical data should be checked for the selected voltage, colour and operating pattern.
Confirm:
- Nominal operating voltage
- Permitted voltage range
- Current consumption for the selected mode
- Control-panel or relay capacity
- Whether the mode is fixed or internally selectable
- Whether remote switching between modes is required
- Required fault monitoring or end-of-line arrangements
Check the ordered variant: a product family may offer several modes, but this does not necessarily mean that every configuration can change modes remotely while in service.
Does the Signal Mode Affect Hazardous Area Suitability?
The visual signal alone does not determine whether a beacon is suitable for an explosive atmosphere. The complete certified construction and equipment marking must match the installation.
Check:
- Hazardous area zone
- Gas or combustible-dust group
- Equipment category and equipment protection level
- Explosion-protection concept
- Temperature class or maximum surface temperature
- Permitted ambient-temperature range
- Required ATEX, UKEX, IECEx or destination-market approval
Read more about ATEX and IECEx certification of hazardous area equipment.
The installation zone should also be confirmed using the guide tohazardous area zones and explosive atmosphere classification.
Examples of Steady, Strobe and Rotating Signals
These products illustrate different signal behaviours. The complete technical and certification requirements must still be checked for each application.
Steady Visual Signal
The MEDC FB11 filament and FL11 fluorescent units provide steady illumination for persistent warning or status indication.
View MEDC FB11 & FL11 steady beacons
How Should the Signal Mode Be Selected?
Selection should begin with the hazardous area and site alarm requirements rather than a preference for the most visually dramatic product.
| Requirement |
Signal to Consider |
Reason |
| Persistent equipment or process state |
Steady |
Provides continuous status indication |
| Abnormal condition requiring attention |
Flashing or Blinking |
Changing signal can attract attention |
| Defined high-intensity pulsed warning |
Strobe |
Produces brief and distinctive visual pulses |
| Recognisable moving visual signal |
Rotating |
Creates an identifiable sweeping or sequenced effect |
For the complete selection process, including zone, certification, temperature, voltage and environmental conditions, read How to Select an ATEX Beacon.
Common Signal-Mode Selection Mistakes
Selecting the most intense signal without considering the required alarm meaning
Using several similar flash patterns that personnel cannot easily distinguish
Assuming a rotating LED signal uses a mechanical motor and reflector
Treating an LED strobe as directly equivalent to a xenon flash-energy rating
Ignoring the effect of sunlight, obstructions and mounting height on visibility
Choosing signal mode before confirming hazardous area certification and temperature limits
Should a Visual Signal Be Supported by a Sounder?
A beacon may form only one part of the alarm arrangement. Audible and visual signals are often combined where personnel may not always be looking towards the beacon or where high noise, hearing protection or visibility restrictions affect alarm recognition.
The alarm design should establish whether a beacon, sounder or combined unit is required.
Explore the wider range of hazardous area sounders, beacons and combination units.
Steady, Flashing and Rotating Beacon FAQs
Is a flashing beacon more visible than a steady beacon?
A changing signal can attract more attention, but actual visibility depends on optical output, viewing distance, colour, ambient lighting, mounting position and surrounding visual conditions.
Is a strobe the same as a flashing beacon?
A strobe is a type of flashing signal characterised by brief pulses. The term flashing can also describe slower or less intense on-and-off patterns.
Does an electronically rotating beacon contain moving parts?
Normally, no. Electronically rotating products create the effect by illuminating LED segments in sequence rather than using a motor-driven reflector.
Can one beacon provide several signal modes?
Some LED products provide several internally selectable modes. Confirm whether the selected variant supports the required patterns and whether they are chosen during installation or controlled remotely.
Which mode is best for process status?
Steady illumination is commonly suited to persistent status indication. Flashing or rotating modes may be more appropriate where the condition needs to attract immediate attention.
Does a beacon mode determine its hazardous area zone?
No. Zone suitability is determined by the complete equipment certification and marking, not by whether the visual signal is steady, flashing or rotating.
Need Help Selecting a Beacon Signal Mode?
Send Thorne & Derrick the hazardous area classification, required alarm behaviour, viewing conditions, voltage, colour and installation environment for product selection support.
CONTACT THORNE & DERRICK
Compare Hazardous Area Visual Signal Options
Explore steady, flashing, strobe and rotating signalling devices for Zone 1, Zone 2, Zone 21 and Zone 22 installations.
VIEW THE VISUAL SIGNALLING RANGE
Choosing Between Two Common Electrical Heat Tracing Technologies
Quick Navigation
Self-Regulating vs Constant Wattage Trace Heating: Overview
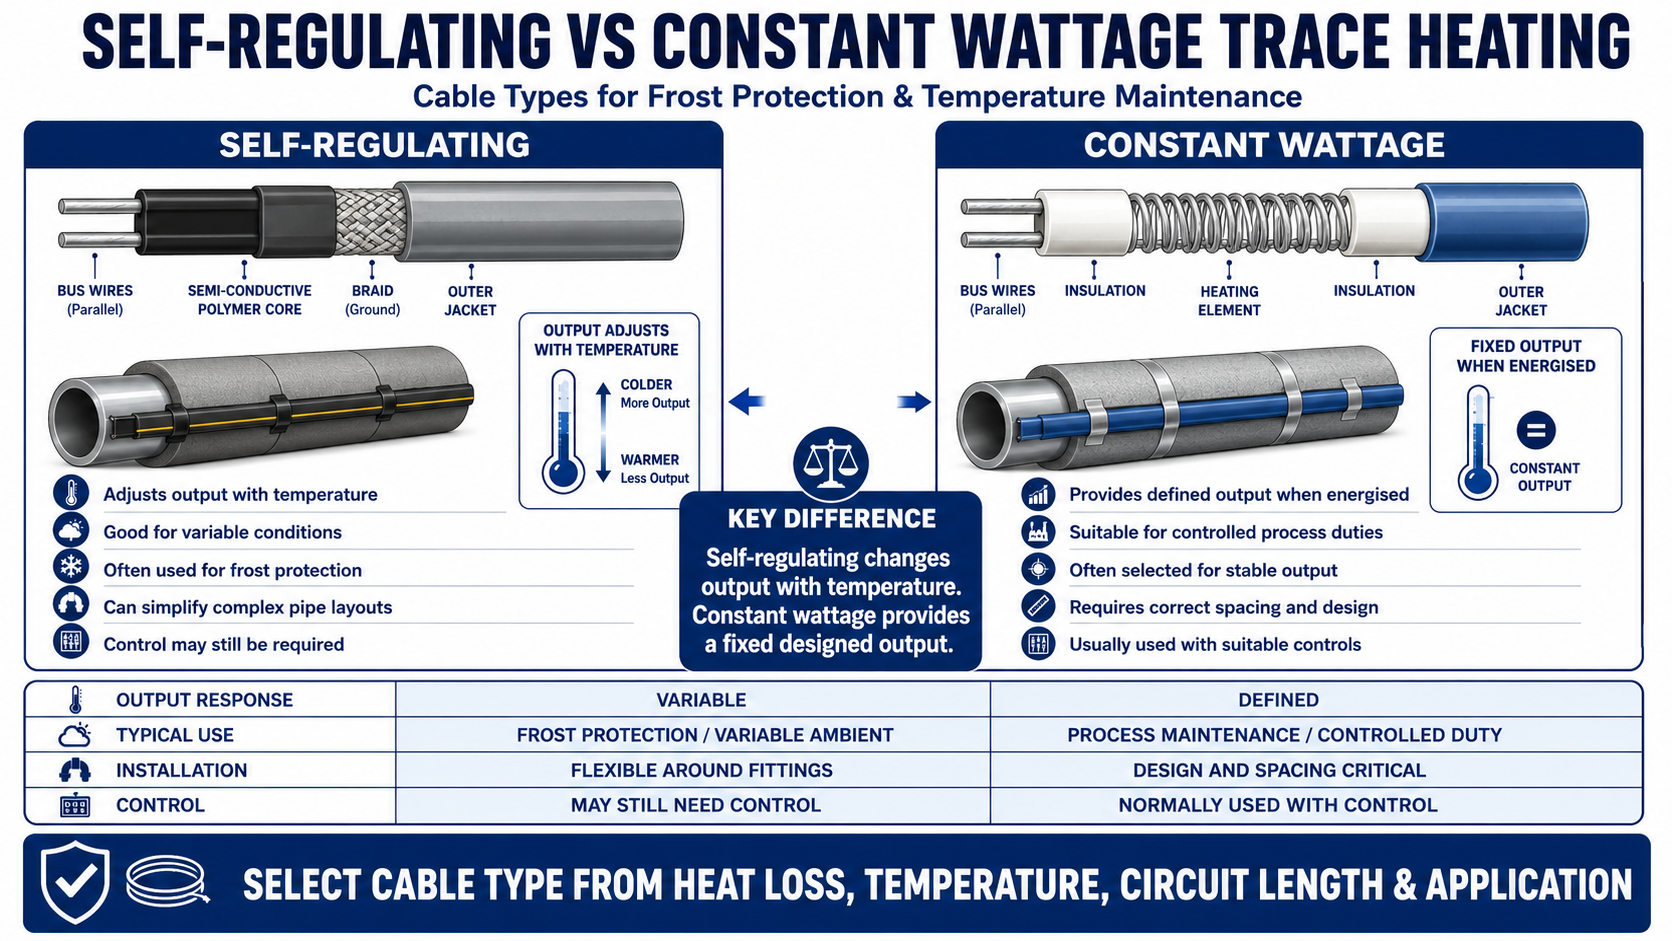
Self-regulating vs constant wattage trace heating is a cable-technology comparison. Both can provide frost protection and process temperature maintenance, but they regulate output differently and have different installation, control and temperature capabilities.
For a broad introduction to the complete system, read how electrical trace heating works. This article concentrates only on the differences that affect cable selection.
The decision should consider:
- Calculated heat loss and required watts per metre
- Maintain and maximum exposure temperatures
- Pipe or equipment material
- Required circuit length and supply voltage
- Need for precise temperature control
- Likelihood of cable crossing or complex fittings
- Safe-area or hazardous-area classification
- Energy, maintenance and lifecycle requirements
What Is the Key Difference?
| Cable Type |
How Output Behaves |
| Self-regulating |
Electrical resistance within the conductive core changes locally with temperature, so heat output increases as the cable cools and decreases as it warms. |
| Constant wattage |
The heating circuit provides a defined output when energised. Temperature is managed through system design and suitable control equipment rather than local self-regulation. |
Important Distinction
Self-regulating does not mean that every system can operate without a thermostat, controller or limiter. Control may still be required for process accuracy, energy management, alarms, equipment protection or hazardous-area temperature classification.
How Does Self-Regulating Trace Heating Cable Work?
A self-regulating cable normally contains two parallel bus wires embedded in a conductive polymer heating core. As the local temperature changes, the resistance of the core changes and alters the heat generated at that point along the cable.
- Colder areas of the cable can produce more heat
- Warmer areas reduce their heat output
- The cable can usually be cut to the required length within its product limitations
- Local output response can help with irregular pipework and changing ambient conditions
- Many products permit limited overlap, but only where the manufacturer explicitly allows it
Explore the available self-regulating trace heating cables for safe-area and hazardous-area applications.
How Does Constant Wattage Trace Heating Cable Work?
Constant wattage cables use a resistance heating element to deliver a defined power output while energised. Parallel-zone designs contain repeated heating zones, while series-resistance cables are engineered to a specific circuit resistance and length.
- Output does not automatically reduce locally as the surface warms
- A suitable control method is normally required
- Parallel-zone cable is cut only at the permitted contact or module intervals
- Series-resistance cable output depends on its designed length, resistance and supply voltage
- Cable crossing or overlap is generally prohibited unless specifically approved
View the constant wattage trace heating cable range for process and industrial applications.
Self-Regulating and Constant Wattage Cable Comparison
| Selection Factor |
Self-Regulating Cable |
Constant Wattage Cable |
| Output response |
Varies locally with cable temperature |
Defined output while energised |
| Cut-to-length |
Usually cut to length within maximum circuit limits |
Parallel-zone types cut at contact intervals; series types are engineered lengths |
| Overlap |
Some products permit overlap subject to instructions |
Normally must not touch, cross or overlap unless specifically approved |
| Temperature control |
May still require control depending on duty |
Normally requires suitable thermostatic or electronic control |
| Complex fittings |
Often convenient around valves, flanges and irregular surfaces |
Requires careful spacing and routing to prevent local overheating |
| Energy behaviour |
Output reduces as the cable warms |
Energy use is governed mainly by output, operating time and control strategy |
| Temperature capability |
Available across low, medium and some high-temperature duties |
Available for wider specialist or higher-temperature duties depending on construction |
| Circuit design |
Maximum circuit length affected by cable, voltage, start-up temperature and protection |
Affected by cable construction, zone spacing, resistance, voltage and control |
| Typical selection reason |
Variable ambient conditions, simple field installation and frost protection |
Stable output, specific process duty or temperature range |
Heat Output and Temperature Control
Neither technology should be selected from its nominal watts-per-metre rating alone. The required output should first be established through a trace heating heat loss calculation.
For self-regulating cable, confirm the output available at the required maintain temperature using the manufacturer’s power-output curves or design software. The nominal output may be stated at a different reference temperature.
For constant wattage cable, confirm that the fixed output and control arrangement can maintain the required temperature without exceeding the pipe, product, cable or area-classification limits.
Control Options
- Ambient-sensing thermostat for basic frost-protection groups
- Pipe-sensing thermostat for direct temperature maintenance
- Electronic controller for improved accuracy, alarms and monitoring
- Independent temperature limiter where a maximum surface temperature must not be exceeded
- Multi-circuit control panel for larger industrial systems
Installation and Circuit Design Differences
Installation convenience depends on the cable construction, pipework layout and approved accessory system.
| Design Point |
Self-Regulating |
Constant Wattage |
| Valves and flanges |
Flexible routing and permitted overlap may simplify allowances |
Spacing and contact must be carefully controlled |
| Branching |
Approved splice and tee components are used where permitted |
Must follow the cable’s zone or circuit design |
| Long circuits |
Maximum length can be limited by start-up current |
Parallel or series designs may suit different long-line duties |
| Termination |
Field termination kits are commonly available |
Termination depends on parallel-zone or engineered series construction |
| Protection |
Circuit-breaker and earth-fault selection must consider start-up behaviour |
Protection must match designed current, output and control method |
| Repair |
Approved field repair systems may be available |
Repairability depends strongly on the cable construction |
Installation should follow the cable-specific instructions and the existing trace heating installation guide.
Typical Applications for Each Cable Type
Self-Regulating Cable Is Often Considered For
- Water-pipe frost protection
- Plant winterisation
- Hot-water temperature maintenance
- Process lines with changing ambient conditions
- Valves, pumps and complex fittings
- Projects requiring cable to be cut from a reel on site
Constant Wattage Cable Is Often Considered For
- Processes requiring defined, uniform heating output
- Higher temperature-maintenance duties
- Longer industrial pipe circuits where a suitable design is available
- Tanks, vessels, silos and specialist equipment
- Applications using detailed thermostatic or electronic control
- Projects where cable construction and chemical resistance match a demanding environment
These are general patterns rather than automatic choices. The correct technology depends on the calculated duty and the performance limits of the individual cable.
Energy Use, Reliability and Maintenance
Self-regulating cable can reduce local output as temperatures rise, but total energy use still depends on cable output, circuit length, insulation, control strategy and operating time.
A constant wattage system can also operate efficiently when correctly sized and controlled. Oversizing either technology or operating it continuously when heat is not required can increase energy consumption.
Lifecycle considerations:
- Quality and condition of thermal insulation
- Accessibility of power connections and terminations
- Availability of compatible replacement components
- Controller accuracy and alarm capability
- Exposure to chemicals, moisture and mechanical damage
- Required inspection and maintenance intervals
Self-Regulating and Constant Wattage Cables in Hazardous Areas
Both technologies may be available as certified systems for explosive atmospheres. Selection must address more than the cable certificate.
- Area classification and equipment protection level
- Gas or dust group
- Temperature class or maximum surface temperature
- Ambient and exposure temperature range
- Approved power connections, terminations, splices and junction boxes
- Control and limiting method
- Installation, inspection and maintenance requirements
See the dedicated ATEX trace heating range for certified cables, controls and components.
Which Trace Heating Cable Should Be Selected?
| Application Characteristic |
Technology Commonly Considered |
| Low-temperature frost protection with variable ambient conditions |
Self-regulating |
| Complex pipe fittings and field cut-to-length installation |
Self-regulating |
| Defined process output with active temperature control |
Constant wattage |
| Higher temperature or specialist industrial duty |
Constant wattage or mineral-insulated, subject to design |
| Very high temperature, high output or severe mechanical environment |
Mineral-insulated may be required |
| Long pipeline |
Cable technology should be selected from heat loss, voltage, circuit length and control requirements |
The table is a starting point only. Product data, design software and technical review are required before final specification.
Information Required Before Comparing Cable Types
Provide the following design data:
- Frost protection or process temperature-maintenance duty
- Required maintain and maximum exposure temperatures
- Minimum ambient temperature
- Pipe diameter, material and length
- Insulation material and thickness
- Valves, flanges, pumps and other local heat sinks
- Available voltage and preferred circuit arrangement
- Safe-area or hazardous-area classification
- Required control, alarm and monitoring functions
- Environmental, chemical and mechanical exposure
Self-Regulating vs Constant Wattage Trace Heating FAQs
Is Self-Regulating Cable Always More Energy Efficient?
It can reduce its local output as temperature rises, but total system efficiency also depends on correct sizing, insulation, control, circuit length and operating time. A correctly designed constant wattage system can also be efficient.
Does Self-Regulating Mean No Thermostat Is Required?
No. A thermostat, controller or limiter may still be required for process accuracy, energy management, alarms, equipment protection or hazardous-area temperature control.
Can Constant Wattage Cable Be Cut to Any Length?
Not always. Parallel-zone cable is cut at defined contact intervals, while series-resistance cable is designed to a specific length and resistance. Follow the individual product instructions.
Can Trace Heating Cable Be Overlapped?
Some self-regulating products allow overlap within their stated limits. Constant wattage and series-resistance cables generally must not touch or overlap unless the manufacturer explicitly approves it.
Which Cable Is Better for Frost Protection?
Self-regulating cable is commonly selected because it responds to local temperature and can be convenient to install. The final choice still depends on heat loss, pipe material, circuit length, environment and approvals.
Which Cable Is Better for High-Temperature Process Heating?
Constant wattage, series-resistance or mineral-insulated cable may offer suitable temperature capability, but the selection depends on maintain temperature, exposure temperature, output, circuit length and environment.
Need Help Comparing Trace Heating Cable Types?
Thorne & Derrick provides heat-loss calculation, cable selection and complete electrical heat tracing system support for frost protection, process maintenance and hazardous areas.
- Self-regulating cable selection
- Constant wattage and resistance cable selection
- Heat-loss calculations and circuit design
- Controls, sensors and temperature limiters
- Safe-area and ATEX component specification
- Complete bills of materials
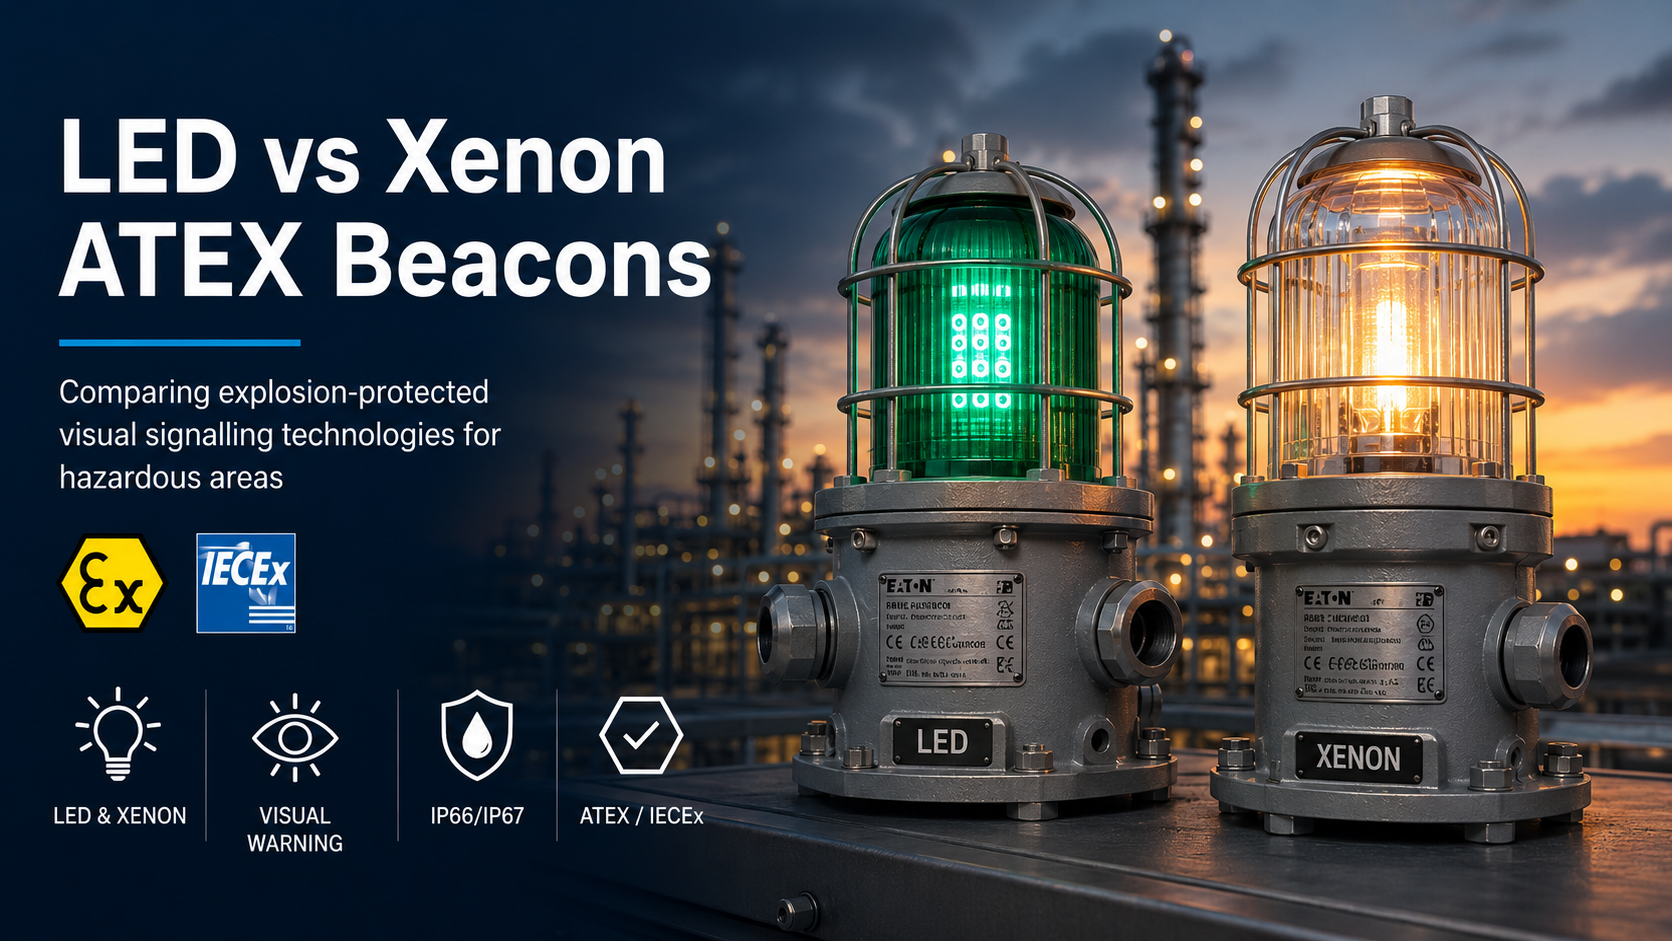
LED and xenon are two of the principal light-source technologies used in hazardous area visual signalling. Both can provide an effective warning, but they produce different signal patterns and are selected using different performance criteria.
An LED ATEX beacon can provide continuous or electronically controlled signalling, depending on the model. A xenon ATEX beacon uses a flash tube to produce a brief, high-intensity pulse and is normally specified by its flash energy in joules.
Thorne & Derrick supplies a comprehensive range of ATEX beacons incorporating LED, xenon, steady, flashing, strobe and electronically rotating visual signals. For a wider introduction to hazardous area visual signalling, read What Is an ATEX Beacon?
Quick answer: select LED where configurable signal modes, continuous indication or long solid-state operating life are priorities. Consider xenon where the specification calls for a defined high-intensity flash measured in joules. Certification and application suitability must be confirmed separately.
LED vs Xenon ATEX Beacons: Quick Comparison
| Selection Factor |
LED Beacon |
Xenon Beacon |
| Light source |
Light-emitting diodes |
Xenon flash tube |
| Typical signal |
Steady, blinking, strobe or electronically rotating, depending on model |
Brief, high-intensity flashing signal |
| Common performance data |
Optical intensity, operating pattern, frequency and current consumption |
Flash energy in joules, flash frequency and current consumption |
| Continuous indication |
Available on suitable models |
Not the normal function of a xenon strobe |
| Configurable modes |
Multiple electronic modes may be available |
Normally a defined flash pattern |
| Service consideration |
Solid-state light source with no xenon flash tube |
Flash-tube operating life should be considered |
| Typical reason for selection |
Flexible signalling, steady status indication or electronic rotating effect |
Defined high-intensity pulsed warning |
Important comparison point: an LED beacon’s optical output and a xenon beacon’s flash energy are not directly interchangeable measurements. A stated number of joules should not be compared directly with a candela or lumen figure.
How Does an LED Hazardous Area Beacon Work?
An LED beacon uses an array of light-emitting diodes to generate the required visual signal. The LEDs may remain continuously illuminated or be controlled electronically to create blinking, pulsed or rotating effects.
The exact capabilities depend on the product. Some models provide only a single steady or flashing output, while others offer several modes selected during installation.
Typical LED Operating Modes
- Steady: continuous illumination for a persistent warning or equipment-status signal
- Blinking: a regular electronic on-and-off pattern
- Strobe: a rapid sequence of electronically controlled LED pulses
- Electronically rotating: LED segments illuminate in sequence to create the appearance of movement
Advantages of LED Signalling
- Multiple signal patterns may be available from one product platform
- Continuous visual indication can be provided
- Solid-state light source with no mechanical rotating assembly
- Suitable for alarm, notification and process-status applications
- Long operating life may reduce routine light-source replacement
These advantages should not be treated as universal. The actual power consumption, visibility, operating life and available modes depend on the selected model, voltage and colour.
How Does a Xenon Hazardous Area Beacon Work?
A xenon beacon stores electrical energy and discharges it through a xenon-filled flash tube. This creates a brief, intense pulse of light.
Xenon strobe performance is commonly described using flash energy in joules and flash frequency. A higher joule figure indicates greater energy released during each flash, but it does not independently determine visibility in every installation.
Advantages of Xenon Signalling
- Produces a distinct high-intensity pulsed signal
- Flash energy can be selected against a defined project specification
- Provides a clearly recognisable strobe-style warning
- Available in different energy, voltage and lens-colour configurations
The flash-tube operating life, current consumption and required energy level should be considered during selection. A higher-energy xenon strobe can require more electrical current than a lower-energy version.
Signal Patterns, Intensity and Visibility
The most important difference between LED and xenon is not simply which technology is brighter. The two technologies communicate visually in different ways.
LED Visual Signals
An LED signal can remain visible continuously or create a repeating electronic pattern. This can make LED suitable for process-status indication, persistent warnings or applications where several different modes are needed.
Xenon Visual Signals
A xenon strobe produces a short pulse followed by a period without illumination. This creates a visually distinctive alarm pattern, particularly where the project specifies a flash energy and frequency.
Site Conditions Affect Visibility
Visibility depends on more than the light source. Consider:
- Viewing distance
- Ambient lighting and direct sunlight
- Mounting height and orientation
- Obstructions, structures and process equipment
- Required field of view
- Lens or LED colour
- Flash or signal frequency
- Site alarm philosophy
Power Consumption, Service Life and Maintenance
Electrical Demand
LED is often associated with lower energy consumption, but this should not be assumed for every hazardous area beacon. Current demand can vary significantly according to voltage, LED colour, signal mode and optical output.
A high-output LED strobe mode may draw more current than a lower-output LED rotating pattern. Likewise, a 15J xenon beacon will normally have different electrical requirements from a 5J version.
The control-panel output, power supply, relay capacity, cable size and voltage-drop calculation should use the data for the exact ordered configuration.
Light-Source Life
LEDs are solid-state components and are frequently selected for applications where long service life and reduced routine replacement are priorities.
Xenon flash tubes have a stated or expected operating life based on the number of flashes. The anticipated alarm duty and testing schedule should therefore be considered.
Inspection Requirements
Neither technology removes the need for hazardous area inspection and maintenance. The enclosure, cable entries, seals, fasteners, lens, guard, earthing arrangements and equipment marking must remain in serviceable condition.
Does Lens Colour Affect LED and Xenon Performance?
Yes. The signal colour can affect the apparent output and visibility of both technologies.
Some LED products use coloured LEDs with a matching or transparent lens. Xenon products normally use a broad-spectrum flash tube with a coloured lens or dome.
Manufacturer performance data should be checked for the exact colour. The intended meaning must also be established by the site alarm philosophy or project specification rather than assumed from the colour alone.
Does the Light Source Affect ATEX Certification?
LED or xenon technology does not independently determine whether a beacon is suitable for a hazardous area. The complete certified product construction must be assessed.
Check:
- Hazardous area zone
- Gas or combustible-dust group
- Equipment category and protection level
- Protection concept
- Temperature class or maximum surface temperature
- Permitted ambient-temperature range
- Required ATEX, UKEX, IECEx or destination-market approval
Read the H&P guide to ATEX and IECEx certification of hazardous area equipment.
Should You Choose an LED or Xenon ATEX Beacon?
Consider LED When:
- A steady or persistent indication is required
- Several selectable electronic modes are beneficial
- An electronically rotating signal is required without moving components
- Long solid-state operating life is a project priority
- The signal is being used for both alarm and process-status functions
Consider Xenon When:
- The project specifies a flash energy in joules
- A distinct high-intensity pulsed warning is required
- The existing alarm philosophy is based on xenon strobes
- A defined flash frequency is required
- The supply and control system can support the required current
Neither technology is universally better. The correct choice is the one that satisfies the hazardous area specification, signal requirements, viewing conditions, electrical design and maintenance strategy.
For a complete step-by-step selection process, read How to Select an ATEX Beacon.
LED and Xenon Product Comparison: Eaton FHF dSLB20
The Eaton FHF dSLB20 family provides a useful example of the practical differences between the two technologies.
Eaton FHF dSLB20 LED
Provides steady, blinking, strobe and two electronically rotating operating patterns. It is suitable where configurable visual signalling is required.
View the Eaton FHF dSLB20 LED signal light
These examples do not replace product selection. Confirm the complete certification, temperature range, voltage, current, colour and installation requirements for the ordered version.
Common LED and Xenon Selection Mistakes
Comparing xenon joules directly with LED candela or lumen figures
Assuming LED always has lower current consumption
Selecting the highest-output product without assessing the viewing conditions
Choosing the lens colour before checking the site alarm philosophy
Assuming the same hazardous area certification applies to every voltage or product variant
Ignoring the ambient-temperature limits associated with the required temperature class
Information Required Before Selecting LED or Xenon
Hazardous area zone
Gas or combustible-dust group
Temperature class and ambient range
Required signal pattern
Viewing distance and ambient lighting
Required lens or signal colour
Operating voltage
Available control-panel current
Indoor, outdoor or offshore conditions
Mounting and cable-entry requirements
LED vs Xenon Beacon FAQs
Is an LED beacon brighter than a xenon beacon?
Not necessarily. The two technologies produce different signal characteristics and are often specified using different measurements. Compare the manufacturer’s optical data, signal pattern and intended viewing conditions.
Does LED use less power than xenon?
It can, but this is not universal. Current consumption depends on the product, voltage, LED colour, signal mode and required output. Use the exact electrical data for the selected configuration.
Can an LED beacon reproduce a xenon strobe?
Some LED products provide a strobe-style electronic pattern. However, its optical characteristics are not automatically equivalent to a xenon flash with a specified energy in joules.
Which technology requires less maintenance?
LED is frequently chosen for long solid-state light-source life. Both technologies still require routine hazardous area inspection, functional testing and enclosure maintenance.
Can LED and xenon beacons be used in the same alarm system?
Potentially, provided the control system supports their voltage, current, monitoring and switching requirements and each product is correctly certified for its installation location.
Which technology is better for a status light?
LED is normally more suited to continuous status indication because suitable products can remain steadily illuminated. A xenon beacon is primarily used for a flashing warning signal.
Need Help Choosing LED or Xenon?
Send Thorne & Derrick the hazardous area classification, required signal pattern, voltage, colour, viewing conditions and installation environment for product selection support.
CONTACT THORNE & DERRICK
Compare Hazardous Area Beacon Technologies
Explore LED, xenon, steady, flashing and rotating signalling devices for Zone 1, Zone 2, Zone 21 and Zone 22 installations.
VIEW THE HAZARDOUS AREA BEACON RANGE
Selecting an ATEX beacon involves more than choosing a lens colour or deciding between an LED and xenon light source. The product must be suitable for the complete hazardous area classification, environmental conditions, electrical system and required visual signal.
The selection process should begin with the hazardous area documentation. The zone, gas or dust group, temperature requirements, ambient conditions and required certification must be understood before comparing individual beacon models.
Thorne & Derrick supplies ATEX beacons for hazardous area visual signalling with LED, xenon, steady, flashing, strobe and electronically rotating options.
For an introduction to their purpose and construction, read What Is an ATEX Beacon?
Selection principle: start with the hazardous area classification and required equipment marking. Signal technology, voltage, colour and mounting configuration should be considered only after the certification requirements have been established.
ATEX Beacon Selection Checklist
1. Confirm the Hazardous Area Classification
Before selecting a beacon, obtain the hazardous area classification for the proposed installation location. This should identify whether the risk relates to gas, vapour, mist or combustible dust and how frequently the explosive atmosphere is expected to occur.
Visual signalling equipment is commonly required in Zones 1, 2, 21 and 22:
| Zone |
Atmosphere |
General Description |
Typical ATEX Category |
| Zone 1 |
Gas, vapour or mist |
An explosive atmosphere is likely to occur occasionally during normal operation. |
Category 2G or equipment providing a suitable higher level of protection |
| Zone 2 |
Gas, vapour or mist |
An explosive atmosphere is not likely during normal operation and, if present, will normally exist only briefly. |
Category 3G or equipment providing a suitable higher level of protection |
| Zone 21 |
Combustible dust |
A combustible-dust atmosphere is likely to occur occasionally during normal operation. |
Category 2D or equipment providing a suitable higher level of protection |
| Zone 22 |
Combustible dust |
A combustible-dust atmosphere is not likely during normal operation and, if present, will normally exist only briefly. |
Category 3D or equipment providing a suitable higher level of protection |
The zone alone is not enough to complete the selection. The gas or dust group, equipment protection level, temperature requirement and ambient conditions must also be confirmed.
Read the H&P guide to hazardous area zones and explosive atmosphere classification.
2. Check the Required Certification and Product Marking
The beacon must carry certification appropriate to the destination market and installation specification. Depending on the project, this may include ATEX, UKEX, IECEx or additional regional approvals.
The complete product marking should be reviewed rather than relying on a general description such as “Zone 1 beacon”.
Equipment Group and Category
The equipment group and category indicate the intended industry and level of protection. Most onshore and offshore processing applications use Group II equipment, but the required category must correspond with the area classification.
Equipment Protection Level
The equipment protection level may be shown using markings such as Gb, Gc, Db or Dc. The required level should be established from the hazardous area design.
Gas and Dust Groups
Gas atmospheres may be classified using groups IIA, IIB or IIC. Combustible-dust atmospheres may use groups IIIA, IIIB or IIIC. The beacon marking must be suitable for the group identified in the site classification.
Protection Concept
Hazardous area beacons can use protection concepts including flameproof, increased safety, intrinsic safety and protection by enclosure. Some products combine more than one concept, such as a flameproof light chamber with an increased-safety terminal compartment.
Read more about ATEX and IECEx certification of hazardous area equipment.
3. Check the Temperature Class and Ambient Range
Temperature requirements are a critical part of beacon selection. The equipment must not create an external surface temperature capable of igniting the identified atmosphere under the certified conditions of use.
For gas applications, the product marking may include a temperature class such as T4, T5 or T6. Combustible-dust equipment is normally marked with a maximum surface temperature in degrees Celsius.
The permitted ambient-temperature range must also cover the lowest and highest expected site temperatures. A product may have different temperature classifications at different ambient limits.
Do not assume: a beacon described as T6 is suitable across its entire published temperature range. The permitted ambient range may reduce as the required temperature class becomes more restrictive.
4. Choose the Required Visual Signal
Once the hazardous area requirements are understood, determine how the alarm or status condition should be communicated.
| Signal Type |
Visual Effect |
Typical Use |
| Steady |
Continuous illumination |
Persistent equipment status, process condition or warning |
| Blinking |
Regular on-and-off light pattern |
Changing condition or attention signal |
| Strobe |
High-intensity pulses |
Alarm or warning requiring a prominent visual signal |
| Rotating |
Moving or electronically sequenced light |
Distinctive warning or plant-status indication |
LED or Xenon?
| Consideration |
LED |
Xenon |
| Signal options |
Can provide steady, blinking, strobe or electronically rotating patterns |
Normally provides a defined high-intensity flash |
| Selection data |
Light output, signal pattern, current and colour |
Flash energy, flash frequency, current and colour |
| Maintenance |
Frequently selected for long operating life |
Flash-tube life should be considered |
| Typical requirement |
Flexible status or alarm signalling |
Prominent pulsed visual warning |
Flash energy or LED technology alone does not establish whether a signal will be sufficiently visible. Viewing distance, lens colour, ambient light, obstructions, mounting height and the site alarm philosophy should also be considered.
5. Select the Lens Colour
Common beacon colours include red, amber, green, blue, yellow and clear or white. The available colours depend on the selected model.
The meaning assigned to each colour should be defined by the site alarm philosophy, operating procedure or project specification. It should not be assumed from the colour alone.
Colour selection can also affect the apparent optical output. Manufacturer performance data should therefore be checked for the exact lens or LED colour.
6. Confirm the Electrical Requirements
Confirm the required supply voltage before selecting the full product reference. Hazardous area beacons can be available in low-voltage DC and mains-voltage AC configurations, but the options vary between models and signal technologies.
Check:
- Nominal operating voltage
- Permitted voltage tolerance or supply range
- Maximum current consumption
- Starting or peak current, where applicable
- Control-panel or relay capacity
- Cable size and terminal capacity
- Earth and equipotential-bonding requirements
- Required switching and monitoring arrangements
Current consumption can vary by voltage, signal mode and colour. The highest applicable value should be considered when sizing the supply and control circuit.
7. Assess the Installation Environment
Hazardous area certification does not automatically establish suitability for every outdoor, offshore or corrosive environment.
Review the following:
- Ingress-protection rating
- Minimum and maximum ambient temperature
- Salt spray, marine or offshore exposure
- Chemical and hydrocarbon exposure
- UV and weather exposure
- Vibration or mechanical impact
- Enclosure material and corrosion resistance
- Requirement for a protective lens guard
IP66 and IP67 are common protection ratings for external hazardous area signalling equipment, but the correct rating should be based on the actual installation conditions.
8. Confirm Mounting and Cable-Entry Requirements
Confirm how and where the beacon will be installed before placing an order. The selected mounting position should provide the required visibility without obstructing access for inspection and maintenance.
Confirm:
- Wall, ceiling, surface or bracket mounting
- Permitted operating orientation
- Required mounting bracket or backstrap
- Number and thread type of cable entries
- Certified cable gland and stopping-plug requirements
- External earth or bonding arrangements
- Required duty or identification labels
- Access for inspection, testing and maintenance
Cable glands, stopping plugs and adaptors must be selected and installed so that the product certification and enclosure protection are maintained.
Example ATEX Beacon Selection Scenarios
The following products illustrate how the required signal type can influence the selection. Complete certification and technical suitability must still be checked for each application.
Configurable Signal Patterns
Where steady, blinking, strobe or electronically rotating modes are required from one product platform, a configurable LED signal light may be suitable.
View the Eaton FHF dSLB20 LED signal light
High-Intensity Xenon Flash
Where a defined xenon strobe signal is required, select the appropriate flash energy, voltage, colour and certified temperature range.
View the Eaton FHF dSLB20 xenon strobe
Information Required to Specify an ATEX Beacon
Providing complete application information helps reduce the risk of selecting an unsuitable product or incomplete ordering code.
Hazardous area zone
Gas or combustible-dust group
Required equipment category or protection level
Temperature class or maximum surface temperature
Minimum and maximum ambient temperature
LED, xenon, steady, flashing or rotating signal
Operating voltage and control arrangement
Required lens colour
Indoor, outdoor, marine or offshore conditions
Mounting and cable-entry requirements
Required regional approvals
Project-specific inspection or documentation requirements
ATEX Beacon Selection FAQs
Can a Zone 1 beacon be used in Zone 2?
Equipment providing a suitable higher level of protection may be acceptable in a lower-risk zone, but its complete certification, environmental suitability and project requirements must still be checked.
Is IP66/IP67 enough for a hazardous area?
No. An IP rating describes protection against ingress but does not replace hazardous area certification. Both the Ex marking and ingress protection must be suitable for the application.
Is an LED beacon always better than a xenon beacon?
No. The correct technology depends on the required visual effect, viewing conditions, flash energy, operating mode, electrical supply and maintenance strategy.
Does the lens colour affect beacon visibility?
Yes. The optical performance can vary by lens or LED colour. Check the manufacturer’s performance data for the exact configuration.
Can the beacon voltage be changed after ordering?
Usually, the operating voltage forms part of the certified product configuration and ordering code. It should be confirmed before purchase rather than changed on site.
Who should install an ATEX beacon?
Installation, inspection and maintenance should be completed by suitably competent personnel using the applicable hazardous area standards, product instructions and site procedures.
Need Help Selecting a Hazardous Area Beacon?
Send Thorne & Derrick the zone, atmosphere, temperature requirements, voltage, signal type, colour and installation conditions for product selection support.
CONTACT THORNE & DERRICK
Compare ATEX Beacon Options
Explore LED, xenon, steady, flashing and rotating visual signalling devices for Zone 1, Zone 2, Zone 21 and Zone 22 installations.
VIEW THE HAZARDOUS AREA BEACON RANGE
Electrical Heat Tracing Inspection, Testing & Troubleshooting
Quick Navigation
Trace Heating Testing, Maintenance and Fault Finding Overview
A reliable trace heating testing programme checks the condition and performance of the heating cable, electrical connections, controls, sensors, insulation and weatherproofing before a fault develops into frozen pipework, lost production or process instability.
For readers who need the underlying operating principles first, see how an electrical trace heating system works. This guide remains focused on inspection, maintenance and fault finding rather than repeating the general definition of trace heating.
The maintenance objective:
- Confirm that the heating cable circuit remains electrically sound
- Identify physical damage, moisture ingress and degraded components
- Verify that controls and temperature sensors respond correctly
- Check that insulation and cladding continue to limit heat loss
- Compare current operating data with commissioning records
- Correct developing faults before cold weather or critical production periods
Safety-Critical Work
Electrical isolation, testing, repair and recommissioning should be completed by suitably competent personnel. Follow the current installation and maintenance instructions for the specific heating cable, connection system, controller and area classification. Do not energise a visibly damaged or unverified circuit.
Why Does Trace Heating Preventive Maintenance Matter?
A trace heating circuit can remain energised while delivering less heat than the process requires. A failed sensor, damaged cable, missing insulation or incorrect controller setting may not be obvious until temperatures fall or a product begins to thicken, crystallise or freeze.
Preventive maintenance helps identify faults while the system can still be inspected, isolated and repaired safely. It also provides evidence that the circuit, control equipment and protective devices have been checked against the design and operating requirements.
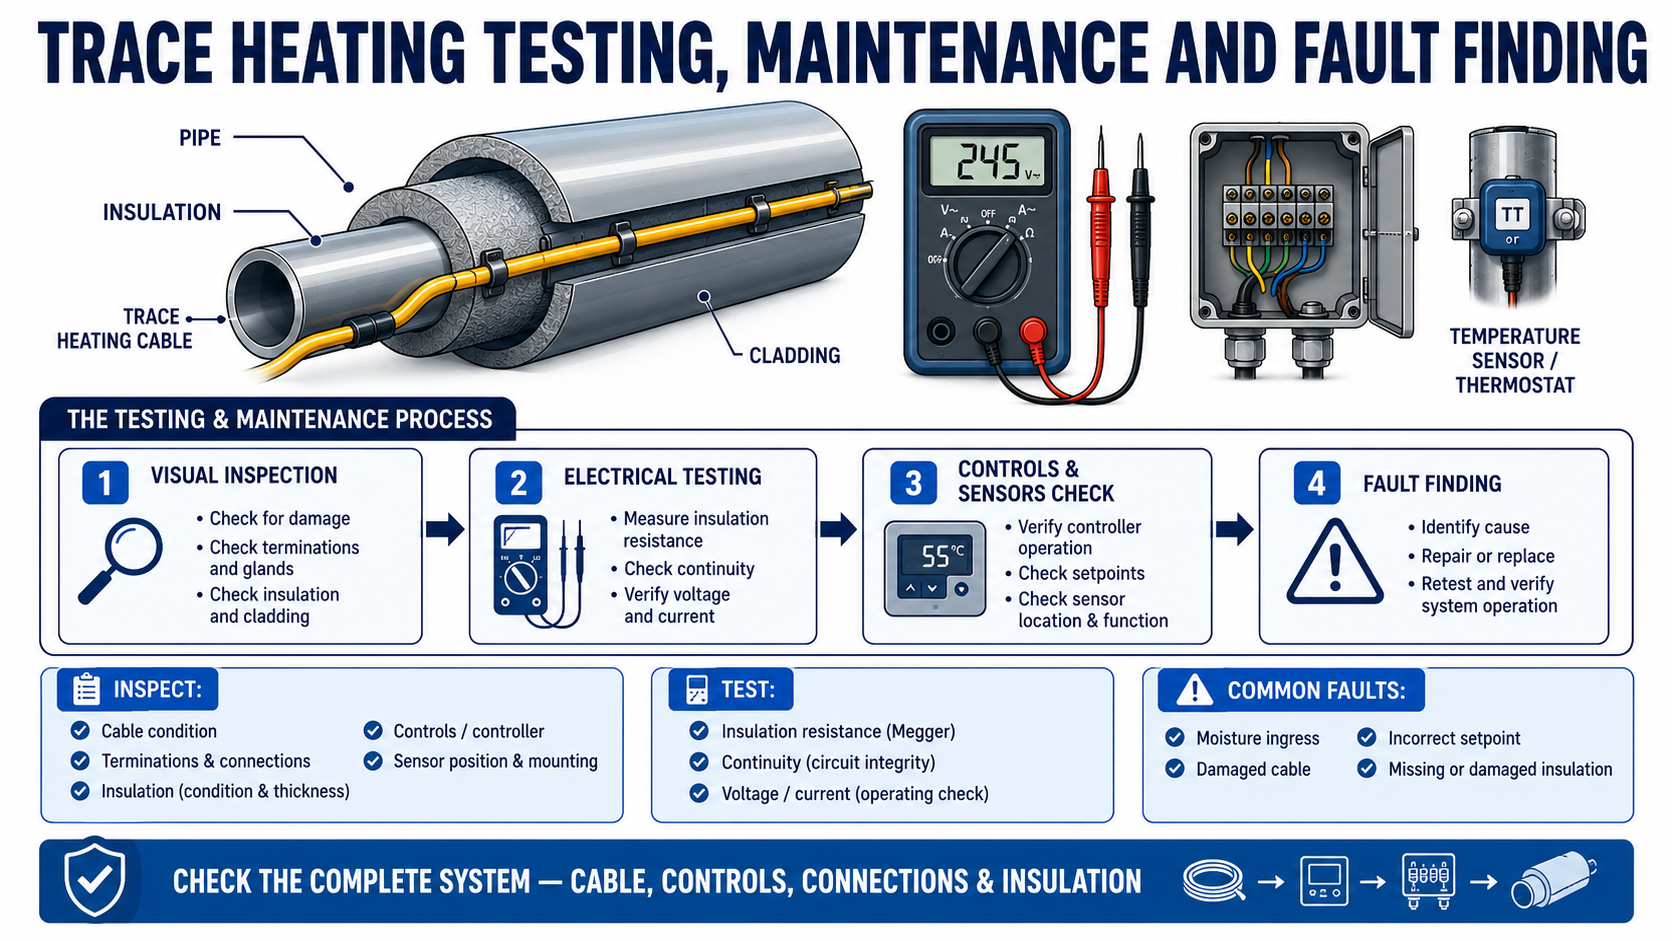
Inspect the Complete System
Cable condition, terminations, controls, insulation and operating data should be considered together.
When Should Trace Heating Be Tested?
Testing requirements vary by manufacturer, project specification, site risk and application. Typical inspection points include:
Recommended test stages:
- When heating cable and components are received
- Before the cable is installed
- After installation on the pipe but before thermal insulation is fitted
- After insulation and weatherproof cladding are complete
- During commissioning before the circuit enters service
- At planned preventive maintenance intervals
- Before seasonal winter operation
- After pipework repairs, insulation removal or maintenance nearby
- After a trip, alarm, unexplained temperature loss or suspected cable damage
The existing trace heating installation guide covers the installation sequence. The checks below focus on maintaining and diagnosing a system once installed.
Safety and Preparation Before Testing
Before opening enclosures, disconnecting circuits or applying test equipment, confirm the site isolation procedure and the limits of the work.
- Identify the correct circuit, cable type and system drawings
- Review the manufacturer’s latest installation and maintenance instructions
- Confirm the supply voltage, protective device and controller arrangement
- Check whether the location is safe or classified as a hazardous area
- Obtain the required permits and verify safe isolation
- Allow hot pipework and process equipment to reach a safe working condition
- Use test equipment suitable for the circuit and environment
- Record ambient and pipe temperatures where they affect the readings
Do Not Use a Universal Pass Value
Insulation-resistance, conductor-resistance and current readings must be assessed against the cable manufacturer’s instructions, circuit length, test voltage, temperature and commissioning records. A value copied from another cable type or project may be inappropriate.
1. Complete a Visual Trace Heating Inspection
A visual inspection should cover all accessible parts of the circuit before electrical testing begins.
| Inspection Area |
What to Check |
| Heating cable |
Cuts, crushing, abrasion, overheating, tight bends, unsupported sections and unauthorised repairs |
| Power connections |
Loose covers, damaged seals, moisture, corrosion, overheating and secure cable entries |
| End seals, splices and tees |
Correct assembly, physical damage, water ingress and compatibility with the cable |
| Junction boxes |
Condition, gland entries, terminals, earthing, identification and enclosure integrity |
| Controllers and limiters |
Display condition, setpoints, alarm status, sensor inputs and signs of overheating |
| Pipe fittings |
Cable routing around valves, flanges, supports, pumps and removable sections |
| Thermal insulation |
Missing, compressed, wet or damaged insulation and incorrectly refitted jackets |
| Weatherproof cladding |
Open seams, damaged seals, missing fasteners and entry points for water |
| Labels and records |
Circuit identification, warning labels, drawings and previous test results |
2. Complete the Required Electrical Tests
The exact test sequence must follow the cable and component manufacturer’s instructions. Common checks include:
Insulation Resistance Testing
An insulation resistance test is used to check the integrity of the cable insulation and jacket system. Readings can be affected by cable length, moisture, temperature, test voltage and the connected equipment, so the approved procedure and acceptance criteria must be used.
Conductor Continuity or Resistance
Continuity and resistance checks help confirm that the heating circuit is complete and that the measured resistance is consistent with the cable type, designed length and temperature. Unexpected readings can indicate an open circuit, short circuit, damaged conductor or an incorrect installed length.
Supply Voltage and Operating Current
Once the circuit has passed the required pre-energisation tests and can be energised safely, measure supply voltage and operating current under controlled conditions. Compare the results with the design information and commissioning record rather than relying on a generic expected value.
Protective Device Operation
Confirm that the circuit protection and earth-fault or residual-current protection are appropriate for the system and have been tested in accordance with the site electrical maintenance procedure.
3. Check Controllers, Sensors and Temperature Limiters
A sound heating cable cannot maintain the correct temperature if its control or sensing system is incorrect.
Controller and sensor checks:
- Confirm the required setpoint and any alarm thresholds
- Check whether the controller is sensing ambient, pipe or product temperature
- Verify that the sensor is in the designed position and securely attached
- Inspect sensor cables for damage and unsuitable routing
- Check displayed temperature against an appropriate reference measurement
- Confirm that outputs switch or modulate as intended
- Test high- and low-temperature alarms where provided
- Verify limiter settings and manual reset functions where applicable
- Review event logs and historical alarm records on monitored systems
For hazardous-area temperature regulation, see the available heat trace thermostats and digital temperature controllers and trace heating temperature limiters.
4. Inspect Insulation and Weatherproof Cladding
Thermal insulation is part of the heating system, not a separate cosmetic layer. Wet, damaged, missing or compressed insulation increases heat loss and can make a correctly powered cable appear undersized.
- Check the full pipe length for missing or displaced insulation
- Inspect cladding seams and penetrations for water entry
- Confirm removable jackets are refitted after valve or instrument maintenance
- Look for crushed insulation at supports and access points
- Check that cable exits and sensor penetrations remain sealed
- Investigate staining, corrosion or ice formation that may indicate moisture
If the original duty or insulation has changed, the system may require a new trace heating heat loss calculation rather than a simple electrical repair.
Common Trace Heating Faults and Likely Causes
| Observed Problem |
Possible Causes |
Initial Checks |
| Circuit will not energise |
Loss of supply, tripped protection, open circuit, failed controller or interlock |
Verify isolation status, supply, protective devices, control demand and circuit continuity |
| Circuit trips immediately |
Damaged insulation, moisture ingress, short circuit, incorrect connection or unsuitable protection |
Keep isolated; inspect components and complete the specified electrical tests |
| Pipe remains too cold |
Insufficient output, missing insulation, incorrect setpoint, poor sensor location, low voltage or damaged cable |
Check heat loss, insulation, controls, voltage, current and installed cable length |
| Pipe becomes too hot |
Incorrect setpoint, failed sensor, bypassed control, excessive cable output or incorrect cable arrangement |
Isolate if unsafe; verify sensor position, controller response and design limits |
| Intermittent alarms |
Loose terminal, moisture, sensor fault, unstable supply or developing cable damage |
Review event history and inspect connections, sensors and cable condition |
| One local area is cold |
Missing cable allowance, damaged cable, displaced insulation or poor cable contact |
Inspect valves, flanges, supports and recently disturbed insulation |
| High energy use |
Incorrect control mode, low setpoint accuracy, wet insulation or unnecessary continuous operation |
Check control strategy, insulation condition, current and operating hours |
A Structured Trace Heating Fault-Finding Process
- Confirm the symptom: establish whether the issue is loss of power, low temperature, overheating, nuisance tripping or an alarm.
- Review the design: identify the cable type, circuit length, required temperature, controls and protective devices.
- Make the system safe: isolate and obtain the necessary permits before intrusive checks.
- Inspect visually: look for damage, moisture, loose connections, missing insulation and recent work.
- Test methodically: complete the manufacturer-specified electrical tests and record every result.
- Check controls: confirm sensor location, measured temperature, setpoints, alarms and output operation.
- Compare with baseline data: use commissioning resistance, voltage, current and temperature records where available.
- Repair with approved components: do not improvise terminations or substitute incompatible parts.
- Retest and recommission: repeat the required tests after repair and update the circuit records.
Building a Preventive Maintenance Schedule
The appropriate maintenance interval depends on the consequence of failure, environmental exposure, process duty, area classification and manufacturer requirements.
| System Condition |
Maintenance Consideration |
| Seasonal frost protection |
Inspect and test before the expected cold-weather period |
| Continuous process maintenance |
Use planned intervals aligned with production and shutdown schedules |
| Harsh outdoor or offshore exposure |
Increase attention to cladding, corrosion, moisture and mechanical damage |
| Frequently disturbed insulation |
Inspect after every intervention involving valves, instruments or pipework |
| Critical or hazardous process |
Use documented risk-based intervals, alarm review and competent technical oversight |
| Monitored multi-circuit system |
Review logged temperatures, current, earth leakage and alarm trends routinely |
Testing Records and System Documentation
Trend information is often more useful than a single isolated reading. Maintain a circuit record containing:
Recommended circuit record:
- Circuit and pipework identification
- Cable manufacturer, type, voltage and designed length
- Power connection, splice, tee and end-seal details
- Controller, limiter and sensor identification
- Design maintain temperature and minimum ambient temperature
- Commissioning insulation resistance and conductor-resistance readings
- Supply voltage, current and pipe temperature at commissioning
- Dates and results of subsequent inspections and tests
- Faults, repairs, component replacements and retest results
- Names or signatures of the competent persons completing the work
Testing and Maintenance in Hazardous Areas
Electrical heat tracing installed in explosive atmospheres requires additional controls over isolation, permits, equipment certification, enclosure integrity, temperature limitation and repair methods.
- Confirm the current area classification and equipment marking
- Check that every replacement component is approved for the cable and location
- Maintain certified glands, seals, enclosures and earthing arrangements
- Verify the designed temperature class and limiting method
- Do not modify certified assemblies outside the manufacturer’s instructions
- Record repairs and recommissioning in the hazardous-area equipment documentation
View the ATEX trace heating systems and components available for hazardous-area applications.
Trace Heating Testing and Maintenance FAQs
How Often Should Trace Heating Be Tested?
The interval should be based on the manufacturer’s instructions, project specification, system criticality, site conditions and risk assessment. Seasonal frost-protection systems are commonly checked before winter, while critical process systems may require more frequent inspection or continuous monitoring.
What Is an Insulation Resistance Test Used For?
It is used to assess the integrity of the heating cable insulation and jacket system. The correct test voltage, connections and acceptance criteria must come from the specific cable manufacturer’s instructions.
Why Is the Trace Heating Working but the Pipe Still Cold?
Possible causes include damaged or missing insulation, an incorrect setpoint, poor sensor location, insufficient cable output, low supply voltage, local heat sinks or a change in the process duty. Electrical operation alone does not confirm adequate thermal performance.
Can Damaged Trace Heating Cable Be Repaired?
Some cable systems have approved repair methods and components, while others require replacement of the affected section or complete circuit. Repairs must follow the manufacturer’s instructions and be retested before energisation.
Should a Self-Regulating Cable Still Be Controlled?
Self-regulating output responds locally to temperature, but controls may still be needed for energy management, process accuracy, alarms, safety or hazardous-area temperature limitation. The system design determines the control method.
What Records Should Be Kept After Fault Finding?
Record the fault, visual findings, test equipment, readings, repair method, replacement components, final retest results and recommissioning data. Update drawings and cable schedules where the circuit has changed.
Need Support with Trace Heating Testing or Fault Finding?
Thorne & Derrick supports the specification, replacement and upgrade of electrical heat tracing cables, controls and connection components for commercial, industrial and hazardous-area systems.
- Heating cable and component identification
- Replacement cable and termination selection
- Controller, sensor and limiter specification
- System design review and heat-loss recalculation
- Support for frost protection and process maintenance
- Safe-area and ATEX product selection